Labeling a silicone baking mat “dishwasher safe” does not mean it will wash clean like new under every operating condition. High-fat foods, cooking sprays, dishwasher cycles, and post-wash storage methods all influence whether a surface develops grease buildup, retained odors, or a sticky feel. Each symptom points to a different underlying cause.
When troubleshooting, first verify whether brand-new parts feel greasy, smell, or feel sticky out of the box. Then record whether these defects return after cooking, washing, drying, or oven bake-off trials. This systematic check determines whether to adjust operating conditions, run cleaning validation, or pause sample approval for factory retesting. A general compliance certificate cannot explain every functional defect.
At YueHouDZ, we produce compression-molded silicone parts and support projects from silicone product design and custom silicone mold manufacturing through prototype validation. For kitchenware brands, sample approval requires more than a simple dishwasher-safe claim. You must define contact foods, oil usage, wash cycles, and acceptance criteria in black and white. That keeps material quality issues separate from everyday user handling.
Dishwasher Safe Does Not Guarantee Clean Results
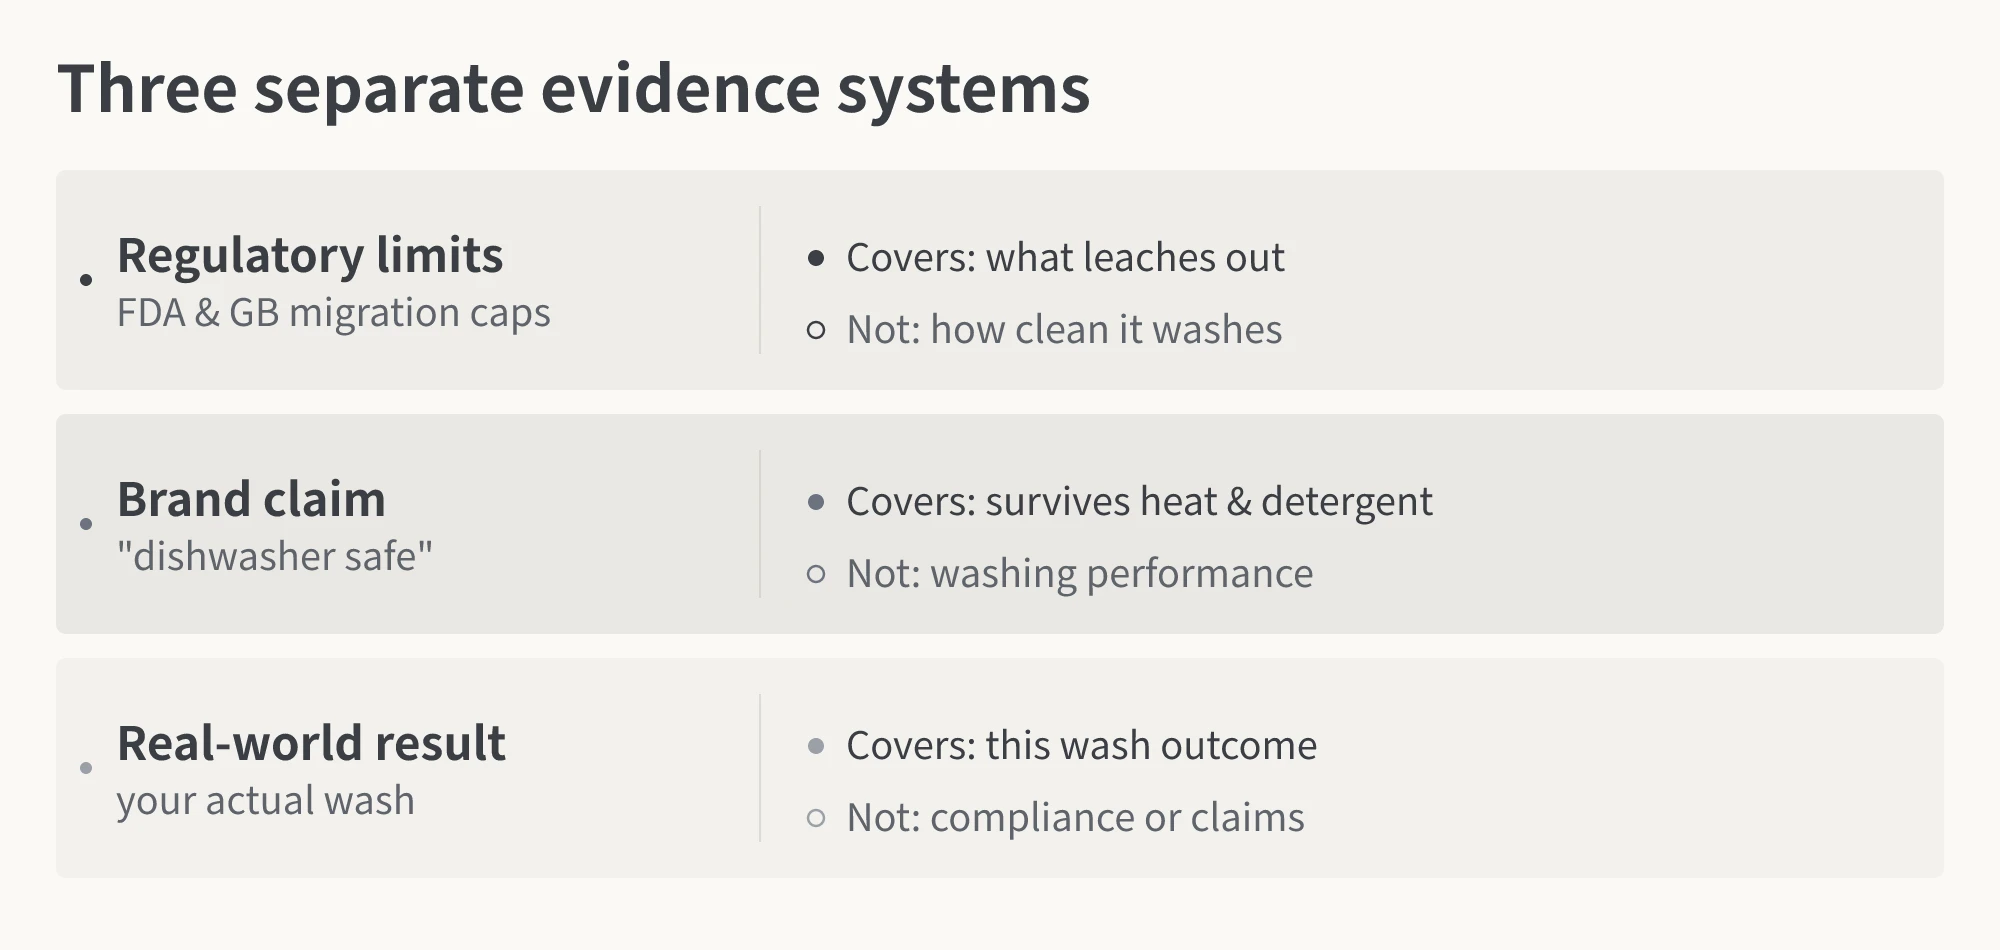
“Dishwasher safe” is not a standardized universal benchmark. It cannot serve as a blanket promise across different brands. Detergent brand Finish notes in its official guidance that dishwasher safety lacks a unified industry definition; manufacturers validate products using their own internal methods. For any specific product, actual operational limits depend strictly on its label, official user manual, and supporting test logs. For example, Fat Daddio’s lists warm soapy handwashing and top-rack dishwasher cleaning as equal options for its silicone mats, advising thorough air-drying after use. Still, this guidance does not replace validating actual cleaning performance. A “top rack only” instruction reflects physical placement and distance from heating elements—it does not guarantee the complete removal of oil films, odors, or stains.
Food contact compliance reports address a different technical scope. US FDA 21 CFR 177.2600 sets extraction limits for rubber articles: distilled water reflux extractives must not exceed 20 mg/in² in the first 7 hours, and n-hexane extractives (simulating fat contact) must not exceed 175 mg/in² in the first 7 hours. The initial wash mentioned in the regulation serves as a manufacturing hygiene requirement, not a dishwasher cleaning performance test.
China’s GB 4806.16-2025 standard for food-contact silicone rubber materials and articles also evaluates substance thresholds. These include overall migration into food simulants, heavy metals like lead, and volatile compounds released under heat (capped at 0.5 g/100 g). These material tests do not replace physical sample records showing whether a mat remains greasy, smelly, or sticky after cleaning under a customer’s specific recipes and wash settings.
During sample reviews, keep three distinct document sets on file: material and migration compliance files, dishwasher durability statements, and actual use/wash test logs. Even when the first two are complete, you must still perform the third. If a technical agreement calls for “easy to clean” or “no residue after wash,” list specific test conditions and pass/fail criteria rather than relying solely on raw material test reports.
Separate Grease, Odor, and Stickiness by Observed Symptoms
Classifying defects by observable symptoms works far better than guessing raw material formulations. If a new part arrives with an oily film that returns days after wiping, investigate the material side first. If an oil film builds up only after several baking cycles, examine the cooking oils and operational parameters. Food odors that fade after an oven bake-off differ from chemical smells in new parts. For sticky surfaces, confirm whether the stickiness remains after following the agreed cleaning and drying procedure.
Grease Buildup: External Oil Films vs. Internal Siloxane Migration
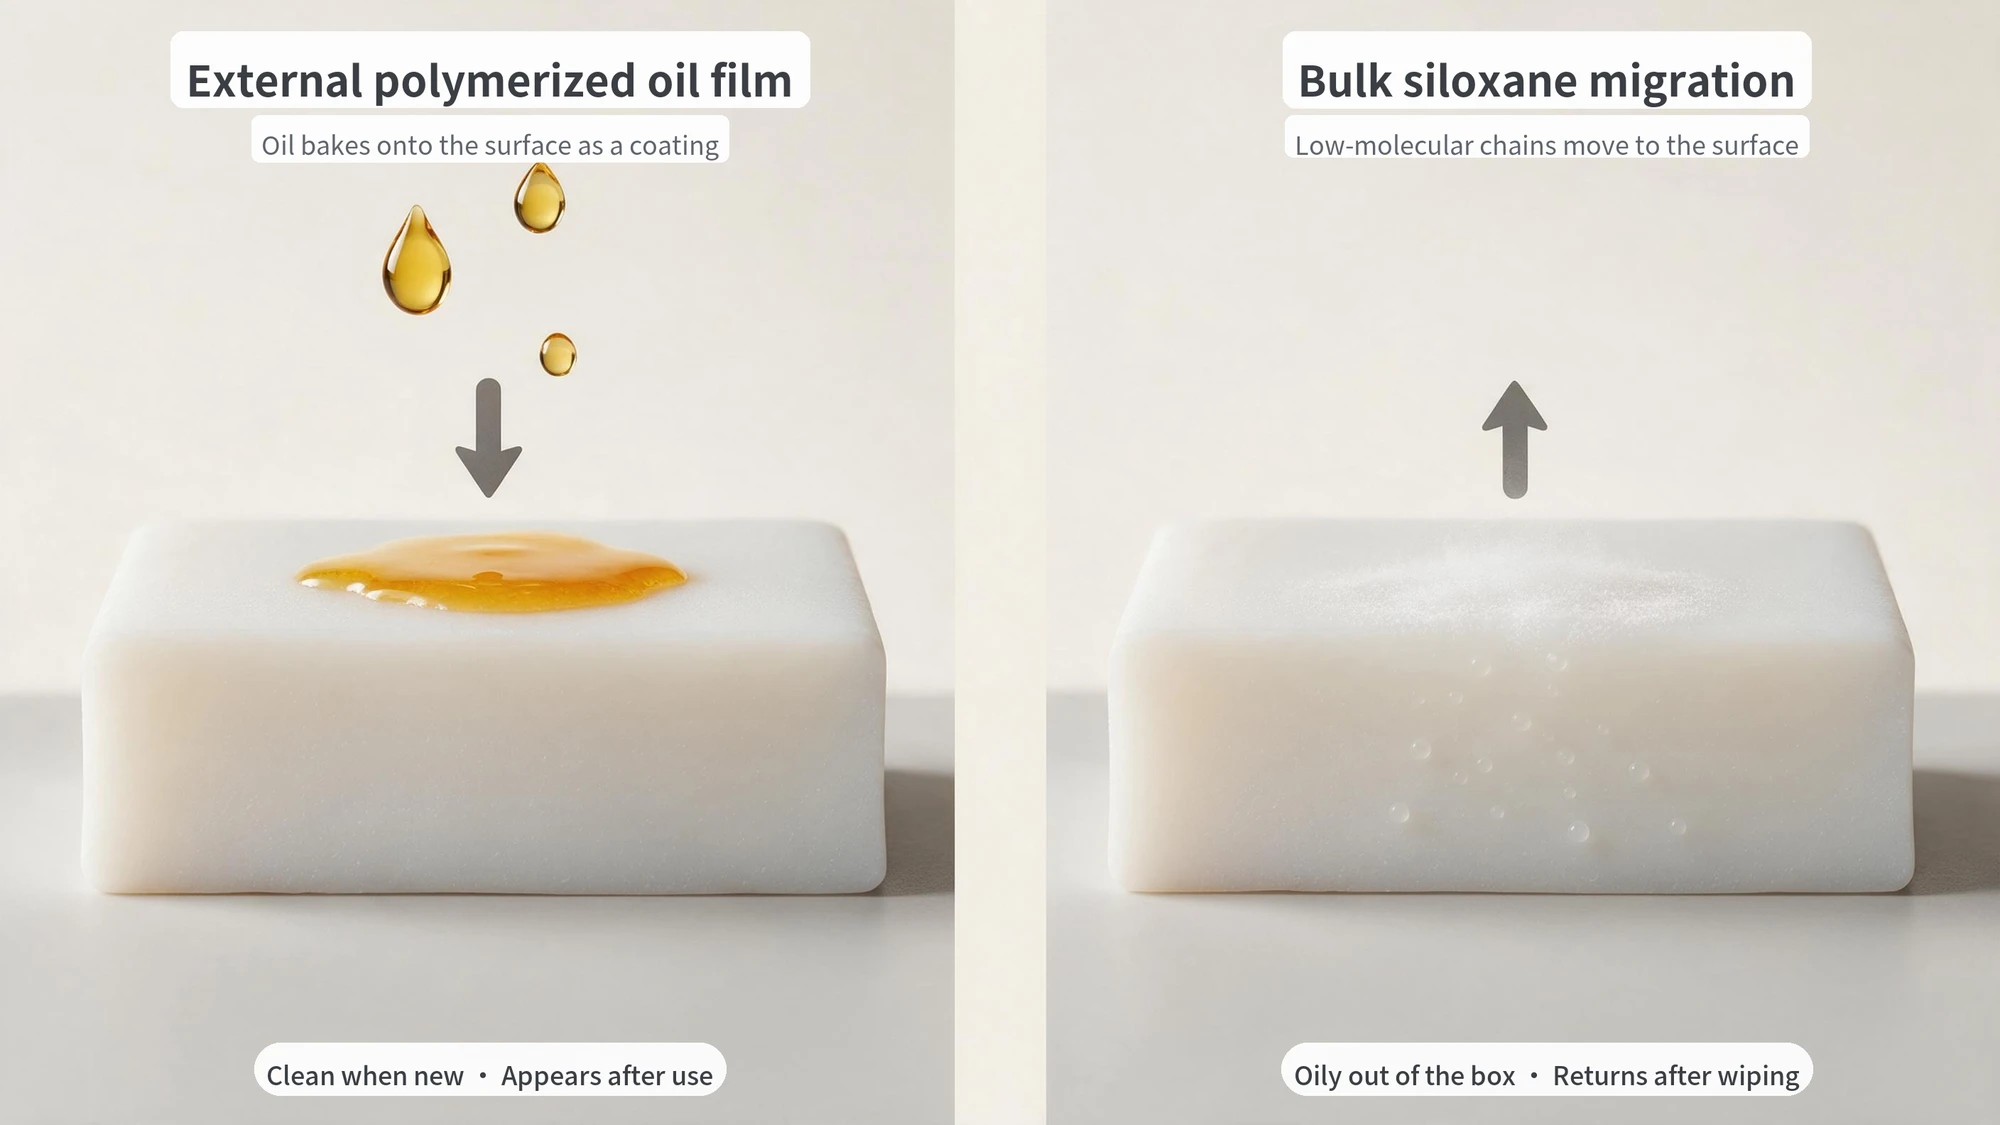
Cooking oils and aerosol cooking sprays cause most surface grease issues during consumer use. Fat Daddio’s silicone bakeware care guidelines note that oils and cooking sprays leave residues that accumulate over repeated use. Baked-on fats and sugars can also turn the surface yellow under high heat. The issue is not simply that silicone absorbs oil. Rather, cooking oils bake onto the surface under high temperatures, making them harder to strip away through routine washing and drying.
On the material side, research confirms that low-molecular-weight siloxanes can migrate in food-contact silicone. If a brand-new part feels oily and the residue returns after wiping, pause sample sign-off. Add compound volatiles, vulcanization parameters, and post-cure processing to your audit checklist, and pull batch records for factory retesting. You cannot confirm the root cause without these records and retests.
Odors: Distinguish Post-Use Absorption from New-Part Chemical Residues
Do not dismiss post-cooking food smells as poor washing. US consumer review outlet Wirecutter noted that silicone traps odors much like flypaper. Wirecutter found that oven bake-out reduced trapped odors, though it found no formal scientific studies explaining the mechanism. Treat this bake-off method as a test option in sample logs rather than a universal standard for all silicone products.
Log chemical odors on brand-new parts separately. China’s GB 4806.16-2025 standard added volatile substance limits, highlighting volatile residues as a key control point for food-contact silicone. If a new sample has a noticeable chemical smell, ask the factory to verify its curing and post-processing setup. Peroxide cure systems produce byproducts that typically require post-cure (a secondary oven baking stage after molding to remove residual volatiles). Platinum cure systems yield different byproduct profiles. Neither cure method guarantees grease-free or tack-free performance on name alone without finished-part testing.
Record storage conditions as well. Stacking silicone mats before they dry completely can intensify odor retention. Control this variable during tests, though it does not explain every odor issue on its own.
Stickiness: Washable Residue vs. Permanent Surface Breakdown
Do not blame stickiness on raw materials right away. If the surface recovers after the agreed cleaning procedure, log it as external residue. Then examine the cooking oils, cycle settings, and detergent dosing. If a new part feels sticky out of the box or stays sticky after repeated cleaning under standard conditions, halt approval and request a factory retest. Fat Daddio’s treats a surface that remains sticky, dull, or loses release properties as a signal for replacement. That supports the rule that permanent defects cannot be washed away, though final sample scrap decisions must follow contract acceptance terms and retest data.
| Observed Symptom | What to Record First | Primary Investigation Focus | What You Cannot Conclude Directly |
|---|---|---|---|
| New part feels greasy; film returns after wiping | Arrival date, wiping method, return timeframe | Raw compound, vulcanization, post-cure | Cannot identify specific formulation flaws from touch alone |
| Oil film builds up after repeated use | Food types, cooking spray use, baking/washing parameters | External grease residue and washing conditions | Cannot declare material non-compliant without testing |
| Retained odor after use; changes after bake-off | Odor source, bake-off settings, reduction degree | Post-use absorption and storage conditions | Cannot treat bake-off results as a universal guarantee |
| Chemical odor or persistent stickiness on new parts | Out-of-the-box condition, post-wash state, recurrence | vulcanization, post-cure, material retesting | Cannot substitute a general material certificate for batch retesting |
Document Test Conditions in Writing Instead of Verbal Notes
The same baking mat can yield completely different results when you change foods, oil application, wash cycles, or storage methods. Logging these parameters lets you isolate variables and determine exactly what caused a failure.
Use the tracking template below for sample validation cycles. Set the cycle count based on product tier, real-world customer usage frequency, and technical agreements. Run initial trial cycles on early prototypes, then reproduce full cycles on release-ready samples as agreed with the buyer. Cycle counts represent specific project test designs, not mandatory industry benchmarks.
| Per-Cycle Log Items | Recommended Entries |
|---|---|
| Sample Identity | Sample ID, batch number, arrival condition, pre-wash photos |
| Cooking Conditions | Food category, brushed/sprayed oil, baking temperature, and duration |
| Cleaning Parameters | Hand wash or dishwasher, rack position, cycle program, detergent brand/dose, and water source |
| Drying & Storage | Full air-dry status, storage method, interval between cycles |
| Visual & Tactile Findings | Greasiness, odor, stickiness, color shift, or surface changes; log as “None / Slight / Severe” with photos |
| Recurrence & Actions | Persistence after altering a single parameter: bake-off, rewash, or return for supplier retesting |
Logging these steps enables systematic troubleshooting. If switching the wash cycle or detergent clears the defect, treat it as an operating condition variable. If greasiness, odors, or permanent stickiness persist on new parts across multiple setups, escalate to material and process retesting. If you set up a boiling water control test, standardize the water source in the technical agreement (such as distilled water) to eliminate water quality variables. A boiling test alone cannot prove or rule out siloxane migration.
Turn Subjective Checks into Verifiable Sample Testing Before Release
During initial unboxing, photograph the part, feel the surface, and smell it to check for oiliness, tackiness, or strong chemical odors. If a new part shows defects, do not waste time running full test cycles. Pause sample approval immediately and have the factory check compound lots, vulcanization logs, and post-cure records.
Next, run cycle testing under real-world operating conditions. Avoid treating “10 cycles” or a specific oven temperature as an absolute industry standard. Your technical specification should define the target recipes, oil usage, cleaning methods, cycle counts, inspection criteria, and retest triggers. For odor bake-off trials, reference Wirecutter’s test range of 120 °C to 175 °C for 20 to 40 minutes as a baseline option. Before adopting this method, record its safety and effectiveness on your specific sample rather than turning it into a blanket acceptance threshold for all baking mats.
If you suspect siloxane migration or undercure (incomplete crosslinking where the rubber matrix fails to set fully), have the factory submit a test plan tailored to the compound and part geometry. The test report must detail sample quantity, project-specific baking temperatures, ambient humidity, duration, test parameters, photos, and acceptance criteria. Without these baseline parameters, a report marked “Pass” cannot correlate with real-world customer usage.
YueHouDZ can incorporate these operating conditions into sample validation across Custom silicone manufacturing, mold tooling, prototyping, and mass production handoff. We help provide raw material compliance documents held by material suppliers, including FDA Food Contact Grade Silicone and LFGB Food Contact Grade Silicone certifications. Final finished-part compliance in target markets and agreed wash performance still depend on physical testing of the completed product.
Keep the final decision workflow straightforward: pause for factory retesting if new parts show defects, return greasy residues after wiping, or remain permanently sticky. If issues appear only under specific foods, oils, or wash cycles, isolate and retest those variables. Always maintain compliance certificates and durability claims on file, but never let them replace physical sample logs. This approach turns “dishwasher safe” from a vague marketing claim into verifiable engineering data for your product team.